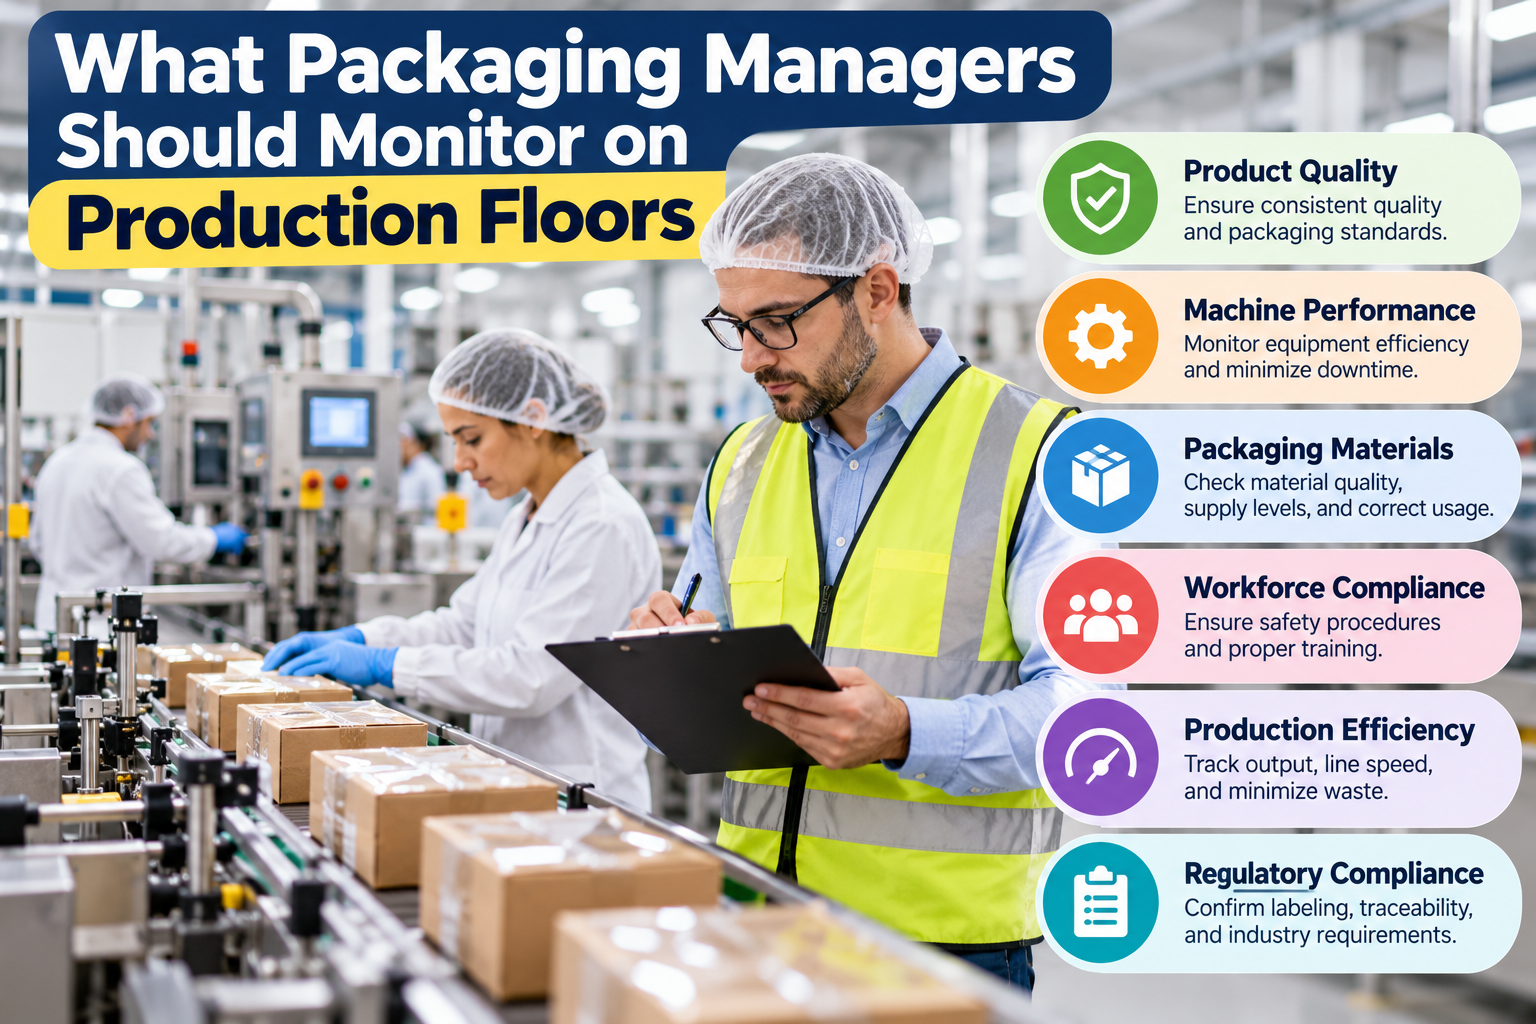
High-speed packaging floors operate on razor-thin margins of time and mechanical precision. When automated conveyors, thermal sealers, robotic palletizers, and vision systems run at hundreds of units per minute, a minor oversight can instantly cascade into a costly production bottleneck.
Effective packaging managers cannot afford to operate reactively by troubleshooting line stoppages after they occur. Achieving high throughput, minimal material waste, and strict quality compliance requires continuous monitoring of operational metrics, material behavior, and ambient environmental variables across every shift.
1. Overall Equipment Effectiveness (OEE) and Micro-Stoppages
Quick Answer: Tracking Overall Equipment Effectiveness (OEE) isolates losses in machine availability, operating performance, and output quality to reveal hidden line capacity.
While total line shutdowns demand immediate attention, minor 15-second sensor trips, bottle tipping, or label misfeeds—known as micro-stoppages—often slip past daily logs unnoticed. Yet, a dozen micro-stoppages per hour consume significant production capacity over a full shift.
Implementing real-time packaging floor OEE tracking helps management separate mechanical failures from operator delays or material inconsistencies. Monitoring OEE at individual workstations pinpoints whether the filler, capper, cartoner, or case packer is acting as the true line bottleneck.
2. Ambient Relative Humidity and Environmental Conditions
Quick Answer: Controlling production floor relative humidity prevents static electricity build-up, cardboard embrittlement, and heat-sealing failures during high-speed packaging runs.
Ambient air quality directly affects raw packaging materials. When factory air grows too dry, static electricity builds rapidly on plastic films, blister packs, and conveyor belts. Static charges cause thin flexible films to cling, jam feed rollers, and attract airborne dust onto clean container surfaces.
Furthermore, low humidity strips moisture from paperboard and corrugated boxes, causing folds to crack during high-speed folding operations. Integrating specialized humidification for the food and beverage industry ensures that primary paper and foil materials retain structural flexibility while protecting delicate food products from premature moisture loss. Establishing consistent packaging line environmental controls eliminates subtle material defects that lead to unexpected machine jams.
3. Material Scrap Rates and Package Seal Integrity
Quick Answer: Monitoring scrap rates and seal integrity catches raw material defects and heater calibration drifts before entire production runs are ruined.
Material waste quickly eats into profit margins. A sudden spike in rejected pouches, crushed cartons, or misaligned labels usually signals an upstream mechanical or environmental issue.
Prioritizing packaging material scrap reduction involves monitoring two critical operational variables:
4. Changeover Efficiency and SMED Metrics
Quick Answer: Measuring changeover duration using Single-Minute Exchange of Die (SMED) principles minimizes non-productive downtime when switching product sizes or formats.
Modern packaging facilities handle an increasing variety of Stock Keeping Units (SKUs). Frequent format changes can destroy daily output if changeovers are unstandardized and unmeasured.
Packaging managers should evaluate:
5. Automated Vision Systems and Code Compliance
Quick Answer: Continuous monitoring of automated vision systems ensures lot codes, expiration dates, and barcodes remain fully legible to avoid costly product recalls.
A beautifully sealed package is useless if the inkjet coder prints an unreadable lot code or misapplies an allergen label. Unreadable barcodes result in retailer chargebacks, while incorrect expiration dates trigger mandatory product recalls.
Managers must regularly audit vision system rejection rates. A sudden jump in vision rejects often indicates a dirty camera lens, slipping conveyor belt, or fading ink printer rather than defective packaging stock.
6. Essential Packaging Floor Monitoring Matrix
Keep this core reference table in mind when auditing daily line performance:
|
Monitoring Category |
Primary Metric |
Common Risk Factor |
Corrective Focus |
|
Line Availability |
Micro-Stoppage Frequency |
Sensor alignment & film jams |
Clear photo-eye lenses; adjust guide rails |
|
Material Quality |
Scrap & Reject Percentage |
Static cling & dry cardboard |
Regulate ambient relative humidity levels |
|
Sealing Operations |
Thermal Seal Bar Temp |
Temperature drift & web tension |
Recalibrate heating elements & tension rollers |
|
Labeling/Coding |
Vision System Pass Rate |
Ink smudging & misapplied labels |
Clean optical lenses & replace printer heads |
|
Format Flexibility |
Changeover Duration (SMED) |
Missing tooling & manual adjustments |
Pre-stage changeover carts; use quick-release mounts |
7. Operator Ergonomic Metrics and Workstation Safety
Quick Answer: Tracking ergonomics and near-miss safety incidents prevents repetitive motion injuries, lowers worker fatigue, and stabilizes line turnover.
High-speed packaging lines rely heavily on human operators for material loading, quality checks, and case packing. Poor ergonomics leads to physical fatigue, which directly increases human error and line stoppages.
Key items to evaluate include workstation lifting heights, repetitive wrist movements at manual sorting stations, and proper machine safety guards. Maintaining a safe, comfortable working environment translates directly into steady production speeds and lower staff turnover.
Managing a successful packaging floor requires balancing machine productivity, raw material behavior, environmental conditions, and operator safety. By moving beyond basic output numbers to actively monitor micro-stoppages, relative humidity, scrap rates, and vision compliance, packaging managers convert reactive troubleshooting into a predictable, highly efficient operation. Small, proactive adjustments made across these critical variables ensure consistent package quality, protect profit margins, and keep lines running smoothly shift after shift.